

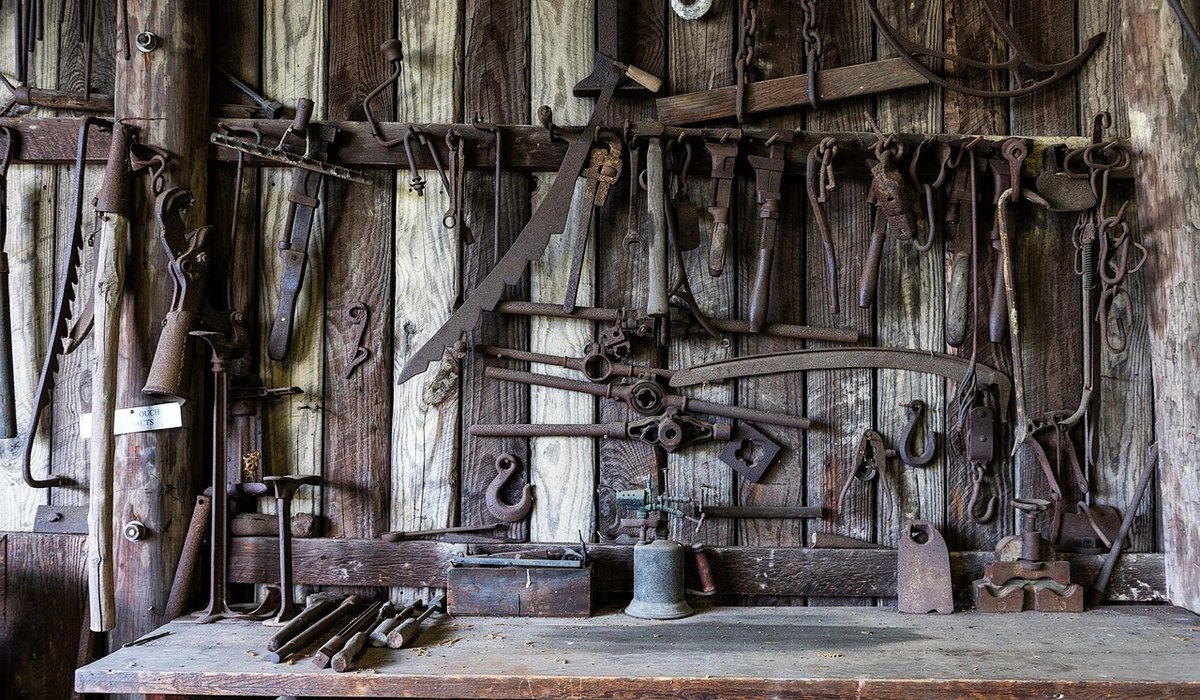
Basic Metallurgy for the Practical Blacksmith
Why metallurgy matters at the anvil
You can spend years learning hammer control, but steel has its own rules. Basic metallurgy is simply knowing what those rules are. It tells you why one bar moves like clay and another fights every blow, why a bright orange heat forgives a sloppy scarf and a yellow heat turns it to sparks. You do not need a laboratory. You need a few ideas: carbon content, grain structure, and the temperature ranges where steel is happiest. With those, you can predict how a piece will behave before you take it from the fire.
Carbon: the quiet ruler of steel
Carbon is the main difference between mild steel and tool steel, and it changes everything. In simple terms, low-carbon or mild steel contains up to about 0.3% carbon. It is soft, ductile, and forgiving. It forges easily, welds beautifully, and will not harden much no matter how you quench it. Medium-carbon steel, roughly 0.3–0.6%, is tougher. It takes a decent edge and can be hardened, but it is less tolerant of rough treatment. High-carbon steel, often 0.6–1.5%, is where knives, chisels, and springs live. It hardens dramatically, holds an edge, and punishes overheating.
- Low carbon: easy to draw out, bend, and forge weld; ideal for gates, brackets, and scrollwork.
- Medium carbon: a useful middle ground for tools that need toughness more than extreme edge retention.
- High carbon: narrow forging range, prone to cracking if worked too cold, and must be normalised before hardening.
- Cast iron: too much carbon, around 2–4%, and not forgeable; it crumbles under the hammer.
A spark test on a grinding wheel gives a clue. Mild steel throws long, straight, straw-coloured sparks with few bursts. High carbon gives shorter, brighter sparks with more forks and star bursts. It is not a precise test, but it trains your eye.
Grain structure: the hidden pattern
Steel is made of tiny crystals called grains. When you heat steel past its critical temperature, those grains change into austenite. If you keep it there too long, or heat it too hot, the grains grow. Coarse grains make steel brittle and difficult to forge cleanly. Fine grains make it tough and predictable. This is why a blacksmith does not simply “get it hot”. You heat to the right colour, work it, and avoid soaking it at welding heat longer than necessary.
Forging itself can refine grains. Each blow breaks up the crystal structure and encourages new, smaller grains to form as the steel cools. But if you finish forging at too low a temperature, you work harden the steel and risk cracks. If you finish too hot, the grains coarsen. Normalising—heating to just above the critical range and letting it cool in still air—resets the grain structure. It is a simple, powerful habit for any smith making tools.
Colour, temperature, and the forge welding window
Colour is your thermometer. In a dim forge, steel tells you its temperature by its glow. These are approximate, because light conditions and alloy content vary, but they are a practical guide:
- Dull red: around 550–650°C. Too cold for heavy forging; bending may crack high-carbon steel.
- Cherry red: around 700–800°C. Near the critical temperature; useful for normalising and some light work.
- Bright orange: around 900–1000°C. The sweet spot for most forging. Steel moves well under the hammer.
- Yellow: around 1100–1200°C. Hot and fast. High-carbon steel can burn here if left too long.
- White: around 1200–1300°C. Forge welding heat. The surface looks almost wet, and a few sparks may fly.
Forge welding happens near the melting point of steel, where the surfaces become plastic and diffuse into one another. Mild steel usually welds around 1200–1300°C. High-carbon steel welds lower, often 1100–1200°C, and is less forgiving. Cleanliness matters: scale, dirt, and oxidation stop the weld. Bring the two scarfed ends to a bright yellow or white heat, dust with borax or a commercial flux, and tap them together with light, rapid blows. Too much heat and you burn the steel; too little and it will not stick.
Reading the steel under the hammer
Once you know carbon and grain, you can feel what the steel wants. Mild steel spreads like warm butter. It tolerates a wide range of temperatures and lets you correct mistakes. High-carbon steel feels stiffer and more resistant. It needs a narrower working range, and it will punish a cold bend with a sharp crack. Medium-carbon steel sits between the two, which is why it is a good choice for punches, drifts, and hardy tools.
Grain structure shows up in the way steel finishes. A piece forged at the right heat has a smooth, almost silky surface under the hammer. A piece forged too hot may look coarse and may tear at the edges. A piece forged too cold develops fine cracks that only appear after quenching. By watching colour and listening to the hammer, you learn to stop before damage begins.
Heat treatment is the final conversation. Hardening requires heating to the correct critical temperature—usually just above non-magnetic for simple carbon steels—then quenching in oil or water. Tempering follows, at a lower temperature, to trade some hardness for toughness. Without normalising first, even a good quench can produce warping or cracks because the grain structure is uneven.
Practise with purpose
Keep a notebook by the forge. Record the steel type, the colour you forged at, and how it moved. Forge test pieces rather than guessing on a finished job. Learn to recognise the moment mild steel turns from orange to yellow, and the moment high carbon starts to sparkle. Normalise your tool steels before hardening. Use flux sparingly and clean your scarfs. Above all, treat every heat as information. The more you pay attention to carbon, grain, and temperature, the less you fight the steel—and the more it works with you.


Forging Basics
-
Combine scrolls, twists, and collars to create gate panels. Learn layout, assembly, and weatherproof finishing for outdoor ironwork.
Projects


-

Long established fact that a reader will be distracted
-

Long established fact that a reader will be distracted
-

Long established fact that a reader will be distracted
Tooling
Karla Gleichauf
12 May 2017 at 05:28 pm
On the other hand, we denounce with righteous indignation and dislike men who are so beguiled and demoralized by the charms of pleasure of the moment
M Shyamalan
12 May 2017 at 05:28 pm
On the other hand, we denounce with righteous indignation and dislike men who are so beguiled and demoralized by the charms of pleasure of the moment
Liz Montano
12 May 2017 at 05:28 pm
On the other hand, we denounce with righteous indignation and dislike men who are so beguiled and demoralized by the charms of pleasure of the moment