

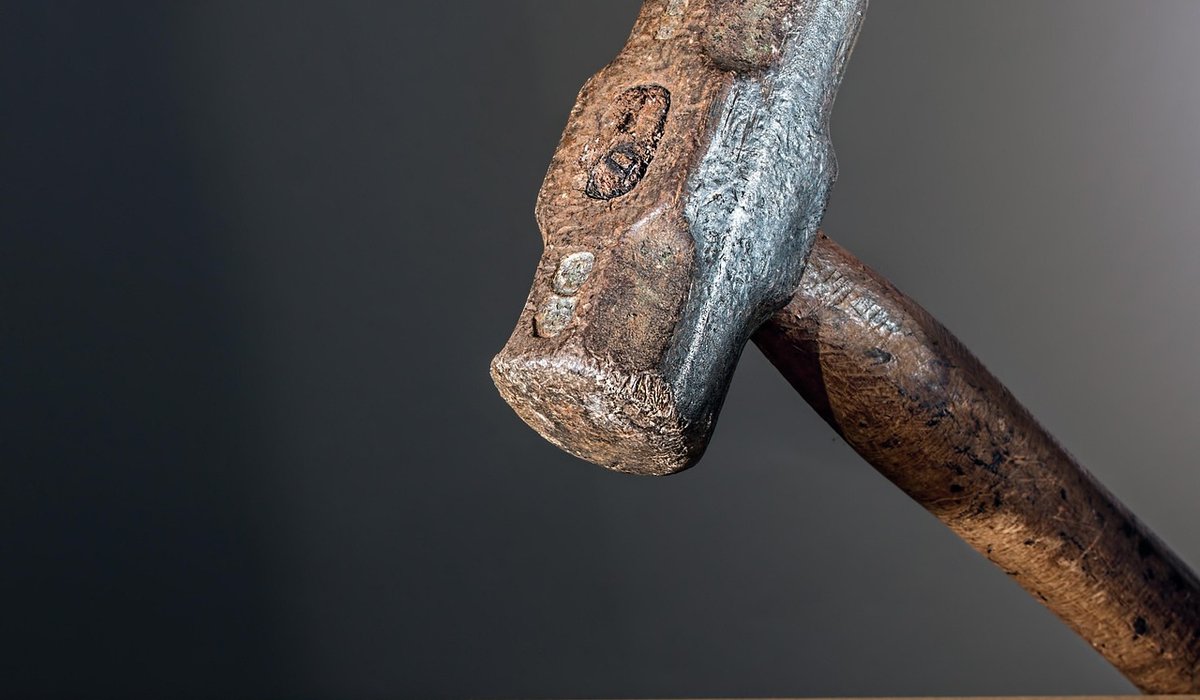
Heat Treating Simple Carbon Steel Tools
Why Heat Treatment Matters
If you have ever forged a chisel from a piece of old file or a length of 1080 bar, you know the moment of truth: tap it into mild steel and watch the edge either bite cleanly or roll over like a piece of tin. That difference is not down to the shape alone. It comes from heat treatment. Hardening gives the steel its cutting ability; tempering gives it the toughness to survive real work. Skip either step and your homemade tool will disappoint you. Get them right and a simple carbon steel chisel or punch can outlast several shop-bought equivalents.
Know Your Steel Before You Start
Heat treatment begins with identification. Simple carbon steels fall into a few broad families, and each has its own quenching speed and tempering range. If you are working with mystery steel, test a small coupon first. A spark test on a grinding wheel will give you clues: short, red-orange sparks suggest low carbon; bright, forked sparks with a bushy end suggest higher carbon. But the only sure way is to harden and break a test piece.
- W1 or 1095: water-hardening. Takes a keen edge, but quench fast and it may crack. Use a warm brine or water quench with care.
- O1: oil-hardening. Forgiving, dimensionally stable, and ideal for chisels, punches and plane irons. Quench in warm oil.
- 5160, EN45 or old leaf spring: tough, medium-carbon. Better for struck tools than fine edges. Temper on the higher side.
Whatever you use, cut a test bar from the same stock. Treat it alongside your tool. When you snap it in the vice, the grain should look like fine grey velvet, not coarse or sandy. That tells you the hardening worked.
Normalising and Annealing
Before hardening, the steel should be stress-free and uniform. Forging leaves internal stresses that can cause warping or cracking during the quench. Normalising is often enough: heat the tool to non-magnetic, about 780–820°C for most simple carbon steels, then let it cool in still air. Do this two or three times. If you need to file or drill the tool after forging, anneal it instead. Pack it in a container of wood ash, vermiculite or lime, heat it to non-magnetic, and leave it to cool slowly overnight. The result is soft, machinable steel that is ready for shaping.
Hardening: Heat and Quench
Hardening is the dramatic part, but it rewards calm, steady work. Heat the cutting end of the tool slowly and evenly. A gas forge or oxy-propane torch works well, but keep the flame moving so you do not burn the steel. Watch the colour: in dim light, non-magnetic occurs around a cherry red, roughly 780°C. Confirm with a magnet. When the steel stops attracting the magnet, it is ready. Do not overheat it to bright orange or yellow; that coarsens the grain and ruins toughness.
- Soak briefly: hold at temperature for 30–60 seconds per 3 mm of thickness. Thicker sections need longer.
- Quench vertically: plunge the tool tip-first into the quench medium. Move it in a gentle figure-of-eight to break the vapour blanket.
- Use the right medium: warm oil (around 50°C) for O1; water or brine for W1 and 1095. Never use cold water on oil-hardening steel.
- Keep it moving: do not let the tool rest on the bottom of the quench tank. That causes soft spots and warping.
As soon as the red colour disappears, pull the tool out. It will be glass-hard and brittle. Do not test the edge yet. Take it straight to the tempering stage.
Drawing the Temper
Tempering removes some hardness in exchange for toughness. It is the difference between a tool that shatters and one that works. The traditional method uses tempering colours, which appear as a thin oxide film on polished steel. Clean the surface first so you can see them clearly. For a chisel or punch, heat the shank away from the edge and let the colours run towards the tip. Stop when the desired colour reaches the cutting edge, then quench in water to freeze it.
- Chisels and carving tools: temper to pale straw or straw, roughly 200–230°C. This gives a hard, long-lasting edge for wood and soft metals.
- Punches and drifts: temper to brown or purple, roughly 230–280°C. They need to withstand hammer blows without mushrooming or snapping.
- Cold chisels for steel: temper to dark blue, around 290–320°C. Softer, but far safer under a hammer.
If you prefer an oven, a domestic oven or toaster oven set to 200–250°C works for small tools. Leave them for one hour, then let them cool in air. For repeatable results, use a thermocouple or an oven thermometer rather than trusting the dial.
Testing, Safety and Finishing
After tempering, test the tool carefully. A file should skate over a properly hardened edge, but bite on the tempered shank. Tap the tool against a brass rod; it should ring, not thud. If the edge chips, temper it a little higher. If it rolls, harden it again and temper slightly lower. Always wear eye protection, leather gloves and a leather apron. Quenching can spit steam and hot oil, so keep a dry powder extinguisher nearby and never quench in a plastic bucket that could soften. Work in a well-ventilated space, and keep water away from molten salt or hot oil. Finally, grind a fresh edge after tempering, taking care not to overheat it. A light hone with a diamond stone will reveal whether your heat treatment has produced a tool worth keeping.


Forging Basics
-
From wire brushing to waxing, finishing protects your work and enhances texture. Explore methods suitable for indoor and outdoor pieces.
Projects


-

Long established fact that a reader will be distracted
-

Long established fact that a reader will be distracted
-

Long established fact that a reader will be distracted
Tooling
Karla Gleichauf
12 May 2017 at 05:28 pm
On the other hand, we denounce with righteous indignation and dislike men who are so beguiled and demoralized by the charms of pleasure of the moment
M Shyamalan
12 May 2017 at 05:28 pm
On the other hand, we denounce with righteous indignation and dislike men who are so beguiled and demoralized by the charms of pleasure of the moment
Liz Montano
12 May 2017 at 05:28 pm
On the other hand, we denounce with righteous indignation and dislike men who are so beguiled and demoralized by the charms of pleasure of the moment