

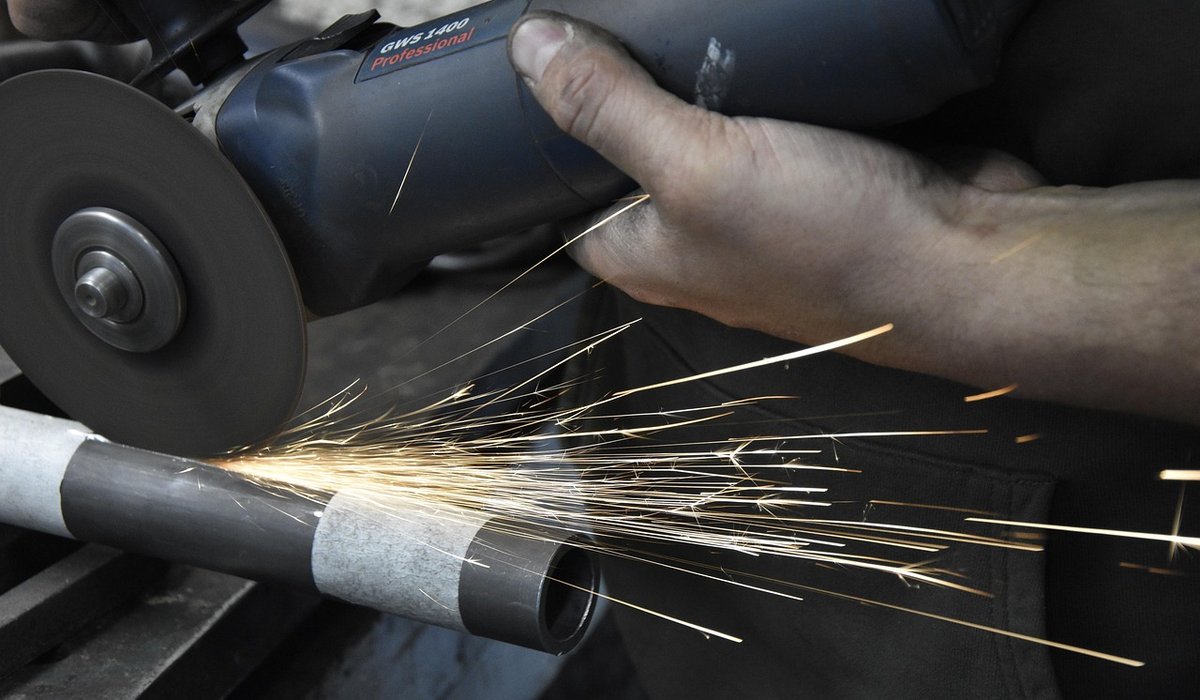
Basic Forging Techniques: Drawing Out, Upsetting and Bending
There is a quiet satisfaction in feeling hot steel yield under your hammer. The anvil becomes an extension of your will, and the fire gives you the power to shape. But before you can forge a scroll or a blade, you need three fundamental techniques: drawing out, upsetting and bending. Master these, and you'll find every subsequent project becomes easier, faster and more precise.
Drawing Out: Stretching the Steel
Drawing out (sometimes called drawing down) is the art of making a piece of metal longer and thinner without losing material. You heat the section to a bright orange-yellow, place it on the anvil, and strike with the face of your hammer. The metal flows away from the blow, lengthening the bar. For efficient drawing, work from the centre of the hot section outwards, turning the bar a quarter turn between blows to keep the cross-section even.
Use the horn of the anvil for sweeping curves and to draw out a taper quickly. The edge of the anvil acts as a fulcrum, allowing you to neck down a section with controlled blows. A lighter hammer gives you more control for fine tapers, whilst a heavier hammer moves metal fast on thick stock. Remember: never hammer below a dull red heat, as the steel becomes brittle and may crack.
- Full-face blows for general reduction.
- Peen blows to spread metal in one direction.
- Anvil step for isolating a section before drawing.
Upsetting: Shortening and Thickening
Upsetting is the opposite of drawing out: you reduce length and increase the cross-section. This is essential for making bolt heads, rivet heads, or thickening a section before bending. Heat the end (or the middle) of your bar to a high yellow-orange. Hold the cool end with tongs, place the hot end on the anvil, and strike the cool end with your hammer. The force drives the hot metal back into itself, swelling it outwards.
Keep the bar perfectly vertical. If it leans, you'll bend it instead of upsetting. For long bars, use an upsetting block or the step of the anvil to support the work. A spring fuller or a guillotine tool can help concentrate the upset exactly where you want it. Upsetting requires more heat than drawing out, so be prepared to return to the forge frequently.
- Heat management: a bright yellow heat upsets best.
- Alignment: any tilt causes bending, not thickening.
- Support: use a block for long stock to prevent whipping.
Bending: Controlled Curves and Angles
Bending hot metal is forgiving and precise. Heat only the area you want to bend to a cherry red. For gentle curves, pull the bar over the horn of the anvil. For sharp right angles, place the hot section over the anvil's edge and strike it down. For tight bends, use a bending fork, a scroll wrench, or the leg vice. Always support the metal on both sides of the bend to avoid kinking.
When bending a taper, forge the taper first, then bend. This prevents the thin end from cooling too fast. For repeated scrolls, make a simple bending jig from mild steel. A common mistake is to bend cold, which risks cracking or uneven curves. If in doubt, reheat. The metal should feel like stiff clay, not like a spring.
- Horn for sweeping, organic curves.
- Anvil edge for clean 90-degree bends.
- Vice for tight, controlled angles.
Heat, Hammer Control and Common Mistakes
All three techniques depend on good heat and hammer control. Mild steel forges best between a cherry red and a bright orange-yellow (around 900–1,100°C). Below a dark red, stop hammering. Your hammer should do the work: grip it loosely, let it fall, and guide it rather than forcing it. Aim your blows so the hammer face strikes flat and true.
Common mistakes include: hammering cold metal, which causes cracks; upsetting a bar that is too long, leading to bending; and drawing out a section too thin before bending it. Another trap is overworking one area until it becomes too cold. Rotate the work, use the whole anvil, and keep your fire clean. A little planning at the forge saves a lot of frustration at the anvil.
Practice Projects to Build Your Skills
Start with a simple taper: draw out a square bar to a point, then bend a small hook. This combines drawing out and bending. Next, make a rivet or a bolt head by upsetting the end of a round bar, then draw out the shank. A classic fire poker uses all three: draw out the tip, upset the handle end for a decorative knob, and bend a scroll for the handle.
Use mild steel (EN3B or similar) for practice. It is forgiving, cheap and easy to forge. Keep your sessions short and focused. Ten minutes of deliberate practice on one technique beats an hour of random hammering. You will soon feel the metal's response and adjust your blows instinctively.
With drawing out, upsetting and bending in your repertoire, you can shape almost any traditional ironwork. The anvil rewards patience and repetition. So light the forge, bring the steel to a bright heat, and let the hammer teach you.


Forging Basics
-
A wall hook teaches tapering, scrolling, and punching. Follow step-by-step instructions to create a useful piece for your home.
Projects


-

Long established fact that a reader will be distracted
-

Long established fact that a reader will be distracted
-

Long established fact that a reader will be distracted
Tooling
Karla Gleichauf
12 May 2017 at 05:28 pm
On the other hand, we denounce with righteous indignation and dislike men who are so beguiled and demoralized by the charms of pleasure of the moment
M Shyamalan
12 May 2017 at 05:28 pm
On the other hand, we denounce with righteous indignation and dislike men who are so beguiled and demoralized by the charms of pleasure of the moment
Liz Montano
12 May 2017 at 05:28 pm
On the other hand, we denounce with righteous indignation and dislike men who are so beguiled and demoralized by the charms of pleasure of the moment